The Comprehensive Guide to Engineered Molded Fiber Packaging.
Moving beyond legacy egg cartons to high-density, thermoformed fiber packaging. Explore mechanical strength, monolithic internal sizing, cold chain thermal curves, and the industrial manufacturing process replacing EPS foam coolers.

The Four Official Molded Fiber Manufacturing Classifications.
The International Molded Fiber Association (IMFA) categorizes molded pulp and fiber into four standardized manufacturing classifications. These types define forming tooling mechanics, de-watering thermodynamics, surface finish, and secondary operations across the global packaging industry.
Type 1: Thick-Wall
Single Mold · Oven Dried
Formed using a single open suction die and deposited directly onto an oven drying conveyor without a mating mold. The part dries via hot-air convection without matched pressing.
- • Tooling: Single open-faced vacuum forming tool with wire mesh screen.
- • De-watering: Free-air hot-convection oven tunnel.
- • Surface: One relatively smooth tool face, one rough unpressed reverse.
- • Tolerance: Plus or minus 2.0 to 3.0 mm; draft angles 3° to 5°.
- • Applications: Heavy industrial dunnage, automotive castings, equipment shipping cushions, nursery pots.
Type 2: Transfer Molded
Dual Mold · Oven Dried
Manufactured using a dual-mold construction: a forming mold collects fiber from slurry, and a transfer mold mates to lightly compress the wet mat and transfer it onto an oven conveyor.
- • Tooling: Forming mold paired with a mating transfer mold.
- • De-watering: Light mechanical transfer press followed by oven tunnel drying.
- • Surface: Tool face is smooth; reverse retains wire screen texture.
- • Tolerance: Plus or minus 1.0 to 1.5 mm.
- • Applications: Egg cartons, fruit and produce trays, drink carriers, consumer electronics protective end-caps.
Type 3: Thermoformed
Cure-in-the-Mold · Matched Heated Dies
Slurry is formed under vacuum, then transferred into matched, CNC-machined heated metal dies (150°C to 200°C). Hydraulic tonnage presses and cures the part directly inside the mold, eliminating drying ovens.
- • Tooling: Matched heated metal dies (male and female) with drainage ports.
- • De-watering: High-pressure in-mold drying via thermal conduction and hydraulic tonnage.
- • Surface: High density, smooth finish on both sides, tight draft angles (1° to 3°).
- • Tolerance: Plus or minus 0.5 mm or tighter, mimicking thermoformed plastic.
- • Applications: Precision consumer goods, electronics trays, cosmetics, foodservice tableware, structural containers.
Type 4: Processed Fiber
Value-Added Enhancements & Barriers
Defined by IMFA as products from Types 1, 2, or 3 that undergo secondary, post-molding, or chemical operations to meet advanced structural, functional, or aesthetic criteria.
- • Hot After-Pressing: Post-cure calibration pressing for ultra-flat sealing flanges and tight friction tolerances.
- • Precision Trimming: Perimeter die-cutting, robotic routing, piercing, or slotting.
- • Functional Barrier Chemistry: Topical spray, dip, or curtain coating for water, oil, and moisture vapor resistance.
- • Furnish Chemistry: Wet-end internal sizing, AKD, and bio-polymer cross-linkers.
- • Decoration: Precision embossing, debossing, dry offset printing, pad printing, or labeling.
How Cold-Chain Shippers Apply the Taxonomy
Industrial packaging engineers evaluate cold-chain shippers by structural integrity, dimensional repeatability, and barrier performance. The RENW Fiber Box does not invent an isolated category. It is an industrial application of Type 3 Thermoformed (Cure-in-the-Mold) substrate manufacturing integrated with Type 4 Processed functional operations:
Type 3 Cure-in-the-Mold Substrate
Virgin cellulose and industrial hemp bast fibers are pressed between matched heated metal dies at 150°C to 200°C under multi-ton hydraulic pressure. This in-mold curing yields a high-density, rigid matrix with 100 kg compressive proof load, smooth two-sided finishes, and uniform draft angles for 5:1 nested storage.
Internal Wet-End Sizing & Finishing
The molded substrate is formulated with monolithic internal AKD wet-end sizing (100% PFAS-free) integrated directly into the fiber slurry, achieving high moisture resistance across humid refrigerated lanes. Automated robotic trim dies then finish the perimeter flange for a 2-piece friction-fit seal that requires zero tape.
Wet Thermoforming vs. Dry Molded Fiber & Extrusion Forming.
Modern packaging engineering is bifurcated between aqueous slurry thermoforming and dry airlaid or extruded continuous fiber converting. Each process operates on distinct fluid mechanics, compaction physics, cycle kinetics, and thermodynamic pathways, establishing explicit boundaries for structural performance and product geometry.
Wet Thermoformed Molded Fiber
Aqueous slurry processing suspends individualized cellulose and hemp fibers in water at 0.5% to 2.0% consistency. Water acts as a lubricating hydraulic medium, enabling fibers to slip and orient in three dimensions across deep cavities under multi-zone vacuum without structural tearing.
Dry Molded Fiber & Extrusion
Dry forming mechanically pulverizes pulp sheets or agricultural fibers into airborne individual fluff fibers with zero liquid water slurry. Fibers are aerodynamically metered into a continuous web or compounded via twin-screw extruders into continuous profile sheets before high-tonnage stamping.
Process Physics & Mechanical Capability Matrix
| Engineering Vector | Wet Thermoformed Molded Fiber (Cure-in-the-Mold) | Dry Molded Fiber (DMF) & Extrusion Forming |
|---|---|---|
| Material State | Aqueous Slurry Suspension (0.5% to 2.0% consistency) Individual fibers suspended in a liquid water vehicle allowing complete 3D fluidic slip and orientation. | Dry Airborne Fluff & Continuous Extruded Web Zero liquid water; aerodynamically metered fluff web or twin-screw compounded continuous profile sheet. |
| Process Water Consumption | 3 to 10 Liters per kg of Finished Fiber Closed-loop water clarification, dissolved air flotation, and internal white water recycling. | Less than 0.1 Liters per kg of Finished Fiber Consumes 90% to 95% less water; eliminates industrial wastewater and effluent permitting. |
| Thermal Energy Demand | High Latent Heat of Vaporization Thermal energy required to evaporate water in-situ as superheated steam during the press cycle. | Low Mechanical Compaction Energy Relies on high mechanical pressure and rapid thermal pulses without evaporating tons of bulk water. |
| Cycle Time | 20 to 45 Seconds per Press Cycle Sequential multi-stage dwell: vacuum preform drainage, die transfer, and in-mold heated cure. | 1 to 3 Seconds per Stroke Continuous web fed through high-speed mechanical indexing or rotary pressing stations. |
| Draw Depth Capability | Deep Draw > 150 to 200 mm Fluidic slip allows complex deep draws with tight vertical draft angles between 1° and 3°. | Shallow Draw < 30 to 50 mm Dry fibers exhibit low elongation before tearing; restricted to shallow trays and low-profile covers. |
| Wall Thickness Range | 2.0 mm to 5.0 mm Structural Walls Heavy-gauge walls engineered for multi-tier stacking loads, puncture resistance, and insulation. | 0.5 mm to 1.5 mm Thin-Gauge Walls Calibrated thin-wall cross sections optimized for single-use lightweight commodity parts. |
| Thermal Insulation | High R-Value Micro-Void Matrix Internal microscopic air pockets within thick walls suppress both conductive and convective heat transfer. | Low Thin-Gauge Insulation Thin solid cross sections provide negligible thermal resistance, unsuited for refrigerated cold chains. |
| Compressive Strength | > 100 kg Proof Load Rating Supports 5-high reefer pallet stacking under dynamic linehaul transit vibrations without failure. | Light-to-Medium Packaging Rigidity Sufficient for edge snap-fit, tray bending resistance, and lid dimensional stability. |
| Prime Industry Roles | Cold-Chain Shippers & EPS Replacement Heavy-duty insulated shippers, meat and fresh seafood transit, and industrial dunnage. | Single-Use Commodities & Blister Packs High-volume hot beverage lids, shallow takeaway trays, cutlery, and retail consumer inserts. |
Material State
Water & Energy Demand
Cycle Time & Velocity
Draw Depth & Wall Caliber
Structural & Thermal Performance
Prime Application Fit
Technical Comparison Matrix: Engineered Fiber vs. Incumbents.
A side-by-side engineering evaluation contrasting thermoformed fiber with functional barrier against the three dominant cold-chain packaging incumbents across physical, logistical, and environmental vectors.
RENW Fiber Box (Thermoformed + Sizing)
- • Thermal Hold: 48+ hours at 0°C to 4°C in refrigerated freight lanes.
- • Compressive Load: 100 kg proof load supporting 5-high reefer pallet stacking.
- • Cube Density: 5:1 compact nesting staging 240 units per pallet footprint.
- • Water Barrier: Monolithic internal AKD wet-end sizing resists moisture in chilled transit.
- • Regulatory: 100% compliant with California SB 54 and Washington RCW 70A.245.
EPS Foam Coolers (Styrofoam)
- • Thermal Hold: Effective insulation, but brittle bead matrix fractures in transit.
- • Compressive Load: 60 to 80 kg proof load; susceptible to sudden puncture.
- • Cube Density: 1:1 rigid blocks staging only 48 units per pallet position.
- • Regulatory: Banned across key states with escalating EPR penalty taxes.
Waxed Corrugated Boxes
- • Thermal Hold: 12 to 24 hours maximum; zero insulation against ambient heat.
- • Compressive Load: Severe wet collapse when moisture dissolves starch glue.
- • Recyclability: Petroleum wax fouls hydropulpers; sent directly to landfill.
Multi-Piece Paper Liners
- • Thermal Hold: 24 to 48 hours; panel gaps cause thermal bypass leaks.
- • Moisture: Vulnerable to edge wicking and internal condensation rot.
- • Operations: Requires warehouse staging and manual insertion of multiple SKUs.
The Industrial Manufacturing Process: Dual-Track Flowsheets.
Commercial molded fiber production executes across two distinct manufacturing disciplines based on geometric draw depth, wall caliber, and production volume. Track A governs aqueous slurry thermoforming for heavy-duty structural containers and cold-chain shippers. Track B governs continuous aerodynamic web and extrusion-style pressing for ultra-high-speed commodity packaging.
Wet Slurry Thermoforming (Cure-in-the-Mold)
Biomass Selection & Slurry Preparation
Virgin FSC-certified wood pulp, industrial hemp bast, and agricultural residues hydrate in closed-loop hydrapulpers at 0.5% to 2.0% consistency. High-precision conical refiners fibrillate cellulose fibers to optimize Canadian Standard Freeness (CSF) and maximize hydrogen bonding without sulfur or chlorine bleaching chemistry.
3D Vacuum Mesh Preform Forming
CNC-machined aluminum forming dies fitted with micro-etched stainless steel mesh screens submerge into the slurry tank. Multi-zone vacuum manifolds draw fibers evenly across 3D contours, forming deep-draw preforms exceeding 150 to 200 mm with tight 1° to 3° vertical draft angles and uniform mat distribution.
High-Tonnage Heated In-Mold Curing
Opposed matched male and female metal dies clamp under 20 to 50+ metric tons of hydraulic pressure at temperatures between 150°C and 220°C. Water flashes off in-situ as superheated steam through micro-exhaust ports, curing and densifying the cellulose matrix into an isotropic rigid structure with internal micro-voids.
Monolithic Wet-End AKD Sizing
100% PFAS-free alkyl ketene dimer (AKD) wet-end sizing is dosed directly into the virgin fiber slurry prior to thermoforming. Monolithic sizing bonds throughout the fiber wall, providing moisture resistance against humid cold rooms and refrigerated condensation without topical plastics or paraffin waxes.
Precision Trimming, Flange Calibrating & 5:1 Nesting
Automated robotic trim dies cut clean perimeter sealing flanges and latching profiles to ensure an airtight friction-fit lid seal without tape. High-speed optical vision systems verify wall thickness, density, and dimensional tolerances before automated arms stack boxes and lids at a 5:1 nested ratio staging 240 units per pallet.
Dry Molded Fiber (DMF) & Continuous Extrusion
Raw Pulp Sheet Infeed & Mechanical Defibration
Commercial cellulose pulp rolls or baled agricultural fibers feed into high-speed hammer mills or disc defibrators. The fibers are mechanically individualized into an airborne dry fluff without the addition of liquid water slurry, eliminating pulping vats and water treatment systems.
Continuous Aerodynamic Web & Extruded Compounding
Airborne fibers are aerodynamically conveyed and metered onto a continuous moving vacuum belt to form a continuous dry fiber web, operating much like a continuous sheet extrusion line. In advanced compounding lines, dry fibers can also be compounded via twin-screw extruders with bio-binders or bio-polymers into continuous profile ribbons or thermoformable sheets.
Rapid High-Tonnage Compaction & Thermal Bonding
The continuous dry web indexes into high-speed stamping or rotary pressing tooling. Clamping pressures up to 40 MPa combined with rapid thermal pulses activate natural lignin glass transition and melt bio-binders in brief 1 to 3 second cycle strokes, consuming up to 90% to 95% less water and minimal drying energy.
In-Line Precision Die Cutting & Barrier Misting
Heated rotary or reciprocating cutting dies trim finished parts from the continuous web at web line speeds. Optional water-based or bio-polymer barrier mists are spray-applied in-line to provide surface grease and moisture repellency for food service items while maintaining clean edge definitions.
Closed-Loop Dry Scrap Recovery & Automated Packout
Skeleton web scrap is continuously vacuum-conveyed directly back to the hammer mill infeed for immediate re-defibration. Because no liquid slurry or wet glue was introduced, dry scrap re-enters the fiber stream with zero material degradation, achieving near 100% raw material yield before automated stacking.
Production overview demonstrating high-precision molded fiber forming, drying, and finishing lines. RENW partners with the PAPACKS platform for North American commercial deployment.
Production Line Stills
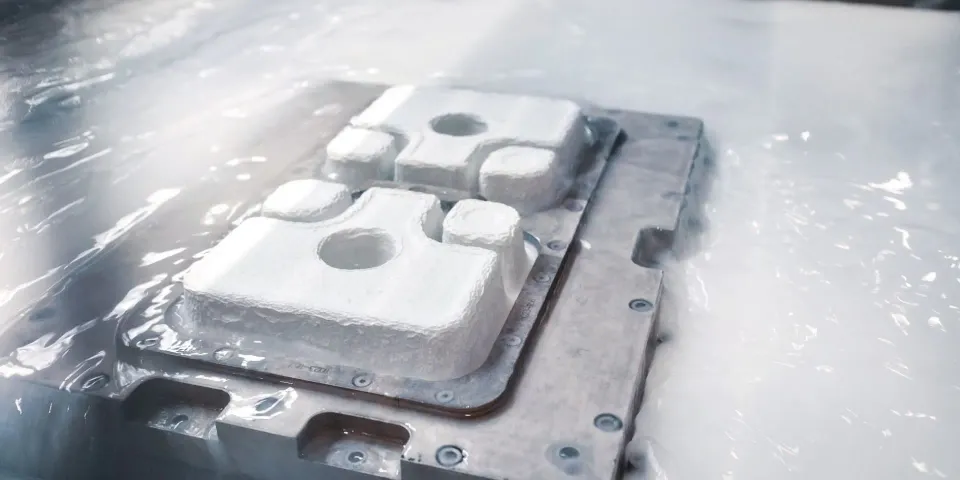
Operational views of pulp suspension mixing, vacuum forming screens, and final curing lines.


Lab Validation: Tested Across Four Physical Axes.
Third-party laboratory testing verifying thermal integrity, mechanical crush resistance, non-wicking water resistance, and standard paper stream repulpability.
48+ Hours at 0°C to 4°C (Reefer Linehaul)
Validated for refrigerated linehaul trailers and cold-room transit profiles. When packed with commercial gel packs or chilled packouts, the container maintains interior payload stability between 0°C and 4°C across multi-day refrigerated transit routes.
- Standard Test Profile:
- Reefer Cold Chain Transit Evaluation
- Payload Stability:
- 0°C to 4°C Across Chilled Linehaul
- Approved Refrigerants:
- Commercial Gel Packs, Soaker Pads, Chilled Packouts
100 kg Compressive Proof Load Rating
Engineered high-density walls and reinforced corner radii deliver exceptional top-to-bottom compression resistance. Boxes withstand 100 kg proof loading, enabling 5-high pallet stacking inside refrigerated linehaul trailers without corner collapse, sidewall buckling, or bead fracturing.
- Static Proof Load:
- 100 kg (220 lbs) Continuous Stacking
- Reefer Truck Stacking:
- 5-High Full Pallet Staging
- Chilled Strength Retention:
- Over 85% Modulus Maintained in Chilled Transit
Monolithic Internal AKD Sizing
Standard paper and corrugated materials absorb liquid water through capillary wicking. RENW thermoformed fiber is monolithically sized with internal alkyl ketene dimer (AKD) wet-end chemistry that prevents capillary water penetration. Chilled condensation does not soften the box structure.
- Sizing Chemistry:
- Internal AKD Wet-End Sizing
- Moisture Rigidity:
- Resists Humid Cold Rooms & Chilled Condensation
- PFAS & Fluorine:
- 100% PFAS-Free Monolithic Sizing
PTS-RH 021/97 Curbside Repulpable (PAP 21)
Certified repulpable under European PTS Method PTS-RH 021/97 and North American municipal paper recycling streams. When placed in standard blue bins, the box breaks down cleanly in standard hydropulpers into reusable cellulose fibers with zero plastic screen residue.
- Repulpability Rating:
- PTS-RH 021/97 Certified Paper Repulpable
- Material Classification:
- PAP 21 Standard Cardboard & Paper Stream
- End-of-Life Destination:
- Standard Municipal Blue Curbside Bin
Frequently Asked Technical Questions.
Technical answers to critical procurement, mechanical, and regulatory questions from enterprise packaging engineers and logistics operators.
How does molded fiber achieve thermal insulation comparable to EPS foam? expand_more
Engineered molded fiber achieves thermal insulation through high-density cellulose walls that trap micro-pockets of air within the dense fiber matrix. Cellulose fibers exhibit naturally low thermal conductivity. When pressed with precision tooling and sealed with engineered friction-fit lids, the container eliminates convective air exchange and thermal bridging. In temperature-controlled linehaul cycles, Type 3 thermoformed fiber containers hold cargo temperatures between 0°C and 4°C across multi-day refrigerated freight routes using commercial gel packs and absorbent soaker pads.
What is the difference between wet thermoformed molded fiber and dry molded fiber or fiber extrusion? expand_more
Wet thermoformed molded fiber utilizes an aqueous slurry suspension where individual cellulose fibers are suspended in water at 0.5% to 2.0% consistency. This allows fibers to flow and slide over each other under vacuum into complex, deep-draw three-dimensional geometries exceeding 150 to 200 mm with tight draft angles. The preform is then cured under continuous hydraulic pressure between heated metal dies at 150°C to 220°C, flashing off water as superheated steam. This forms a structural, high-density matrix with micro-cavities that deliver superior thermal insulation (high R-value) and compressive proof loads exceeding 100 kg, making it mandatory for heavy cold-chain shippers. In contrast, dry molded fiber mechanically defibrates pulp sheets into airborne fluff with zero water slurry, aerodynamically metering fibers onto a continuous moving vacuum belt or compounding them through twin-screw extruders into continuous profile sheets. High-speed indexing presses then compact the dry web at extreme pressures up to 40 MPa with cycle times of 1 to 3 seconds, using rapid thermal pulses to bond fibers. Because dry fibers lack the fluidic slip of water slurries, dry forming is restricted to shallow draws under 30 to 50 mm and thin walls between 0.5 and 1.5 mm. It uses 90% to 95% less water and minimal thermal drying energy, making it optimal for high-volume single-use items such as beverage lids, shallow trays, and blister packs.
Can molded fiber hold fresh seafood in commercial refrigerated lanes? expand_more
Yes. The Fiber Box utilizes internal AKD (alkyl ketene dimer) wet-end sizing integrated directly into the thermoformed cellulose substrate. When paired with commercial gel packs and absorbent soaker pads in refrigerated reefer lanes (0°C to 4°C), it resists ambient moisture and protein drip without structural collapse or floor delamination throughout linehaul distribution.
Is modern molded fiber packaging truly curbside recyclable? expand_more
Yes. Unlike waxed corrugated cardboard, plastic-lined foam coolers, or foil-insulated paper bags, RENW engineered molded fiber is certified 100% repulpable under European PTS-RH 021/97 and North American recyclability test protocols. It contains zero polyethylene films, zero petroleum wax, and zero persistent microplastics. End-users can place the entire box directly into standard curbside blue bins with ordinary paper and cardboard waste.
How does 5:1 nesting save warehouse and freight costs? expand_more
Rigid EPS foam coolers are molded as fixed blocks that cannot nest, forcing logistics operators to pay to store and transport empty air at a 1:1 ratio. A standard 48-inch by 40-inch pallet position accommodates only 48 assembled foam coolers. In contrast, RENW thermoformed fiber is engineered with precise draft angles that allow tight 5:1 nesting. The identical pallet position stages 240 complete units, reclaiming up to 80% of warehouse floor space and eliminating 4 out of every 5 inbound truckloads.
Does RENW molded fiber contain PFAS or fluorinated chemicals? expand_more
No. RENW molded fiber packaging is 100% free of per- and polyfluoroalkyl substances (PFAS) and contains no intentionally added fluorinated chemicals. Our water and oil barrier systems rely on non-toxic, plant-based organic polymers. All materials comply with California AB 1200, Washington State RCW 70A.245, European Union REACH standards, and FDA 21 CFR Section 176 regulations for direct food contact.
Deploy Engineered Molded Fiber Across Your Logistics Network.
Transition your cold chain away from rigid foam coolers and non-recyclable waxed cartons. Request evaluation samples, review CAD packaging geometry, or schedule an engineering consultation with our team.
Direct Engineering Hotline
+1 (844) 620-RENW
Packaging engineers standing by for cold-chain packout audits, ISTA thermal data sharing, and custom tooling feasibility.